What Does a Certified Reman Build Really Involve?
Intro
Many fleet buyers see the label “certified reman” and assume it means a truck has been fixed, cleaned and tested. This narrow understanding leaves teams vulnerable to vendors selling overhauled or cosmetically refurbished units under the same name.
A genuine certified reman build is a structured, rule-bound manufacturing process, not a one-off repair job. Governed by REMAN ROAD, it follows fixed engineering gates, mandatory inspections and traceable record-keeping. This article breaks down exactly what takes place from the moment a qualified core enters the workshop until the finished truck is handed over to the fleet buyer.
Pre-build core validation
A certified remanufacturing cannot begin with an unvetted core. Before any teardown work starts, technicians carry out intake assessment. Inspectors review the vehicle’s known service history and look for red flags: impact damage, evidence of sustained overload, corrosive exposure, unapproved structural modifications or signs of catastrophic prior failure.
The core must pass this stage. If its structural capacity is already beyond recovery, it is rejected for reman and sent for recycling. Only cores with proven remaining fatigue margin move forward into the build sequence. This remanufacturing step separates compliant certified remanufacturing from rebuilds that start with high-risk, borderline frames and components.
Full disassembly and deep cleaning
Partial disassembly is not acceptable for REMAN ROAD certified remanufacturing builds. Every critical system is completely taken apart down to individual components: frame, axles, suspension, engine, transmission, brake assemblies and hydraulic parts. All components go through industrial cleaning to strip grease, carbon deposits, rust scale and surface coatings.
Cleaning is not just for appearance. It removes surface obstructions so inspectors and NDT equipment can spot hidden cracks, pitting and material loss that paint or grime would conceal. This is one of the most commonly skipped steps in low-quality refurbishment.
Component inspection, NDT and grading
Once clean, each load-bearing and functional part moves to inspection. Dimensional checks verify whether parts stay within OEM design tolerances. Mandatory non-destructive testing including ultrasonic, magnetic particle and radiographic inspection screens for subsurface flaws invisible to the naked eye. Based on test results, every component is formally graded into one of three categories: reusable, repairable or mandatory scrap.
Repairable items can only proceed if remediation follows approved engineering procedures, and they must pass re-inspection afterward. Any part hitting scrap criteria is discarded, no exceptions. Mechanics cannot choose to reuse a defective component to cut costs. All grading decisions are logged and linked to the vehicle VIN.
Controlled restoration and component replacement
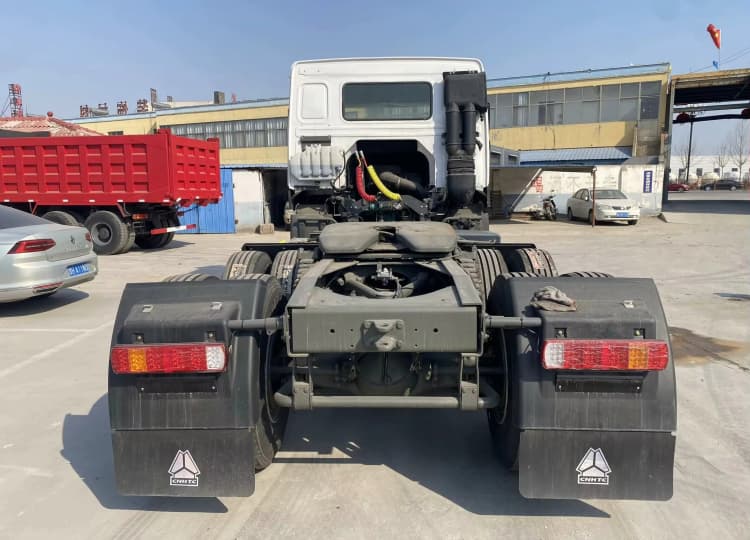
Reusable parts are set aside for reassembly. Repairable parts undergo precision restoration such as machining, journal resurfacing or qualified welding under controlled procedures. Any part marked scrap is replaced, either with another graded reman component or a new OEM-equivalent part.
Standard certified remanufacturing builds automatically replace all time-sensitive wear items: seals, gaskets, bearings, brake linings, hoses and fasteners, even if they appear visually intact. Wear parts have fixed service lifecycles; relying on their remaining unknown life would break the lifecycle-reset principle. This remanufacturing step ensures the finished vehicle starts its new cycle with fresh consumables.
Subassembly rebuild and bench validation
Before the whole truck is assembled, major subassemblies are rebuilt and tested independently on dedicated benches. Powertrain units run on dynamometers to verify power output, torque curves and temperature stability. Hydraulic assemblies go through pressure hold tests. Brake systems are calibrated and checked for response, leakage and performance thresholds.
Bench testing is component-focused and runs under controlled load conditions, far more rigorous than a brief road test. Failures are fixed at the subassembly stage, rather than being hidden inside a finished vehicle. Only subassemblies that meet the acceptance thresholds move on to vehicle assembly.
Whole-vehicle assembly and system calibration
Qualified components and validated subassemblies are reassembled following OEM assembly specifications and torque standards. This is not casual reassembly. Technicians follow controlled work instructions to restore the vehicle to its original engineering design intent.
After assembly, all interconnected systems are calibrated: engine ECU, braking modules, suspension geometry, hydraulic controls and safety sensors. Mismatched calibration or improper alignment creates hidden reliability issues, even when individual parts are sound. System integration is a critical, often overlooked part of the certified build.
Final vehicle acceptance testing
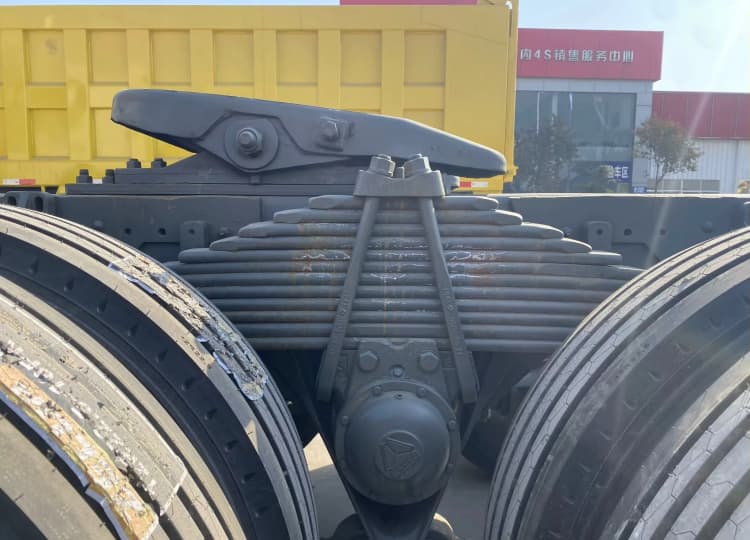
Once fully assembled, the heavy truck goes through a final acceptance protocol. This includes functional system checks and structured road testing under representative load conditions. The goal here is to confirm that all systems work together as an integrated vehicle.
It validates that there are no leaks, abnormal noises, control delays or performance deviations introduced during assembly. Important to note: final testing is confirmation, not the primary quality filter. Most defect screening already happened at component and bench test stages.
Dossier compilation and warranty activation
No ccertified remanufacturing build is complete without a full traceable dossier tied to the VIN. This document package compiles intake screening notes, teardown logs, NDT reports, component grading records, bench test data, calibration sheets and final acceptance sign-off.
The warranty is activated only once the full audit trail is complete. Unlike vague warranties for generic rebuilt trucks, a REMAN ROAD warranty is backed by this documented proof of every quality gate. Buyers receive this dossier at handover for internal fleet records, insurance checks, future audits and resale transparency.
Closing
A certified remanufacturing build is far more than repairing broken parts or refreshing a truck’s appearance. It is a gated industrial workflow: qualified core intake, full disassembly and cleaning, NDT-backed component grading, scrap replacement, independent bench validation, precise assembly, system calibration and fully documented final acceptance.
Every remanufacturing step exists to reset the asset’s lifecycle to a predictable, known performance baseline. When evaluating suppliers, you can use this sequence as your checklist. If any of t