Debunked: Reman Manufacturing Is Just Expensive Repainting
Introduce
One of the most persistent myths in the heavy truck circular market is simple: reman manufacturing is just repainting, overpriced cosmetics wrapped in a fancy technical name. This misunderstanding comes from low-grade vendors who use paint, filler and cleaning to disguise worn, fatigued chassis, then sell the result as remanufactured.
Cosmetic work and certified reman manufacturing sit on opposite ends of the workflow. Painting is a minor, optional final step. True reman manufacturing is a manufacturing-grade reset of the entire asset.
What “expensive repainting” actually is?
Pure cosmetic refurbishment targets only what the eye can see. Work includes surface cleaning, rust sanding, body filler for dents, primer and fresh topcoat, cabin detailing and tire dressing.
Its core limitation: no structural disassembly, no hidden defect inspection, no mandatory part replacement, no system calibration. A thick layer of paint can cover frame cracks, corrosion pits and deformation. It changes appearance, but it does not restore residual fatigue margin or fix degraded internal components.
This process is cheap and fast. It improves curb appeal, but leaves all the underlying mechanical and structural risks untouched. This is the patchwork build that feeds the reman myth.
What certified reman manufacturing actually does before any paint touches the frame?
Painting happens late in the REMAN ROAD reman manufacturing workflow, after all high-stakes technical gates are completed.
First comes core qualification. The full truck is assessed as one integrated asset. Teams review service and overload history, run dimensional checks and deploy NDT scanning across all high-stress structural zones. If fatigue or permanent deformation exceeds the acceptable threshold, the core is rejected. It will not enter reman, no matter how clean it could look after painting.
Next is full disassembly. Every major subassembly, fastener, seal, bearing and wiring harness is separated from the chassis. Components are cleaned, measured, graded and sorted into three groups: regenerable, mandatory replacement, or condemned for scrap.
Machining for reused parts follows strict OEM material-thickness limits. No over-machining to erase wear marks. Replacement parts must match original material specification and heat treatment standards. Generic fit-only aftermarket parts are not accepted without independent validation.
After reassembly, every linked system is calibrated back to OEM design intent. Cooling, brake balance, torque delivery and ECU logic are tuned to preserve the original design margins. Then the unit passes loaded end-of-line testing, simulating real heavy-duty cycles to log temperature peaks, vibration, leak performance and fault behaviour.
Only once the truck passes all engineering validation gates does surface preparation and painting begin. Paint protects the finished asset from corrosion; it does not create the reman value.
The cost difference comes from engineering, not paint
Buyers who see a large price gap between a painted cosmetic truck and certified reman manufacturing often assume the premium goes to paint. That is incorrect.
The real cost drivers are:
- NDT inspection and fatigue assessment
- Full teardown and component sorting labour
- Mandatory replacement of seals, bearings and critical fasteners
- Precision machining and material verification
- System calibration and loaded validation testing
- Permanent VIN-linked traceability documentation
Paint and surface finishing represent only a tiny fraction of the total reman manufacturing investment. A vendor can apply a premium-quality paint job for a relatively low cost, but cannot replicate the structural and system validation that defines certified reman manufacturing.
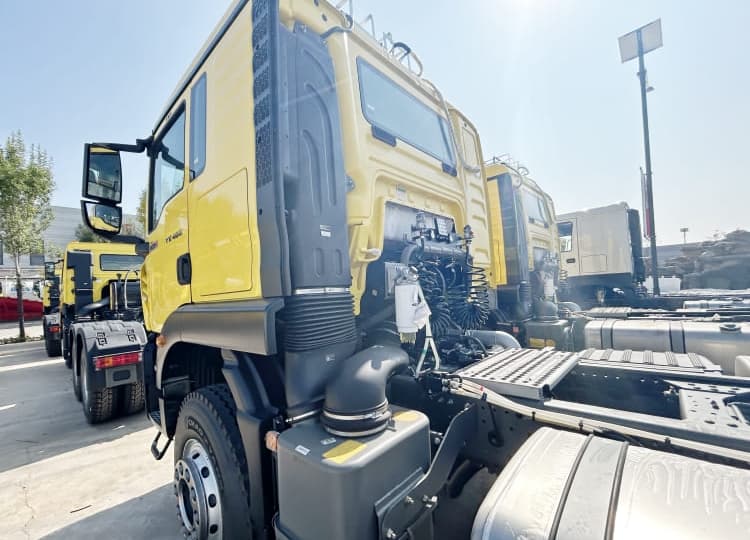
The risk gap: paint hides failure; reman eliminates measurable failure triggers
A cosmetic repaint is designed to hide defects. Frame cracks, hidden corrosion, worn gear clearances and drifting calibration remain, concealed under coating. Failures tend to strike unexpectedly under peak payload or rough terrain.
Certified reman manufacturing is designed to expose defects first. The workflow removes unknown risk by quantifying residual margin, replacing time-sensitive wear parts and proving system harmony. Its whole-vehicle warranty reflects that verified baseline.
This is the critical distinction. Paint is for concealment. Reman manufacturing is for controlled, auditable risk reduction.
How to tell the difference when evaluating suppliers?
Use these simple checks to separate cosmetic builds from genuine reman manufacturing.
- Ask whether NDT fatigue reports and dimensional measurements are available before any rebuild work started.
- Confirm if the scope includes full disassembly, or only surface cleanup and painting.
- Clarify whether replacement parts follow OEM specification or generic aftermarket fitment.
- Check whether final validation is a short static run, or loaded system testing across all linked subsystems.
- Verify that all inspection and part records are locked to the VIN for audit.
A supplier who leads sales conversations with photos of shiny paint, but cannot share structural test data, is selling cosmetic refurbishment.
Closing thought
The myth that reman manufacturing is just expensive repainting survives because bad actors have turned paint into a marketing trick. Fresh paint is not worthless; it protects the asset after reman is finished. But it is never the core work.
True reman manufacturing is a system-level engineering reset. It judges the core on fatigue, disassembly, component control, calibration and validation. Paint is only a finishing step.
Fleet buyers who understand this distinction stop paying reman-level pricing for cosmetic disguise, and focus procurement decisions on the technical proof that guarantees uptime and safety.